



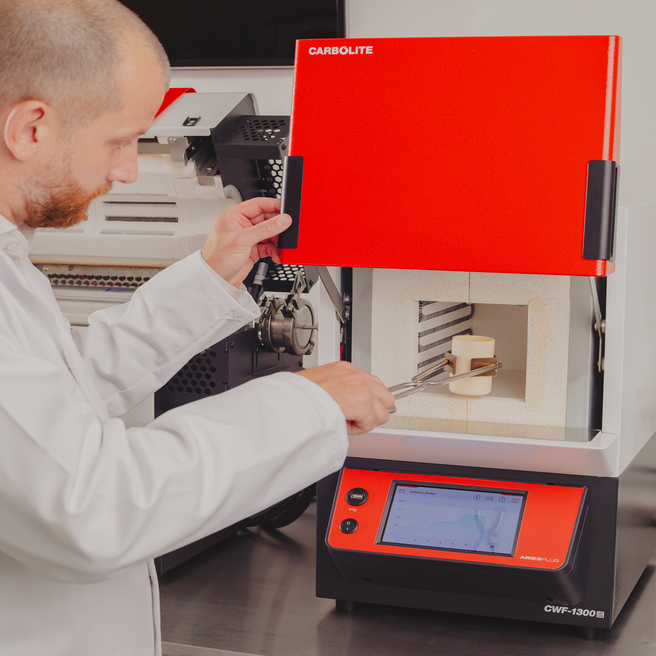
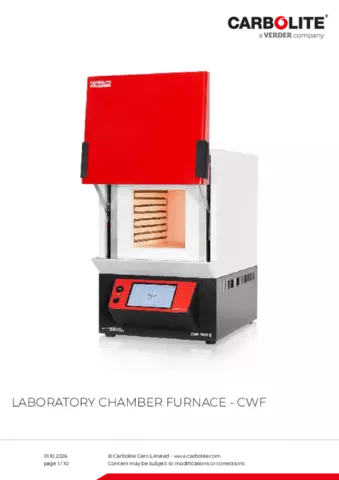
CWFシリーズは卓上タイプの研究用汎用チャンバー炉です。最高温度1300℃で、5種類のサイズからお選びいただけます。
標準仕様
- 常用温度1000℃(最高温度1100℃)、常用温度1100℃(最高温度1200℃)、常用温度1200℃(最高温度1300℃)
- チャンバー容積5L、13L、23L、36L、65L
- Programmable EPC3016P1 controller
- パラレルアクションドアにより高温になったドアの内側がユーザーに向くことはありません
- Soft closing door on 5, 13 & 23 litre models protects the thermal insulation
- 硬質アルミナで、炉入口とヒースも保護されています。
- 高性能断熱材の使用で効率良い昇温・温度維持が可能
- 自然輻射型巻線式ヒータによる最適な均熱性
- 万一ヒーターが故障した際にも、ヒーターユニット部分が容易に交換可能
オプション (注文時に御指定ください)
- デジタル通信オプションに対応した高機能デジタルコントローラ、多段階プログラマ、データロガーを幅広く用意しています(コントローラの詳細については別途ご案内します)。
- 貴重な内容物の保護および無人運転時の安全確保のため、過昇温保護機能を推奨しています。
- 最大1100℃までの改変雰囲気下で使用可能な各種金属製レトルトをラインアップしています。
- AMS2750H(Nadcap)準拠用途向けの特注仕様にも対応可能です。
CWF - 汎用卓上型チャンバー炉(電気炉) 1100°C, 1200°C, 1300°C ATMOSPHERE RETORTS FOR CWF FURNACES
A retort can be used for various heat treating processes requiring a controlled inert or reactive atmosphere, e. g. to prevent oxidisation or to enhance surface hardness. The A105 retort, which incorporates a silicone rubber seal, can achieve low oxygen levels. Manufactured in either NiCr alloy (Inconel) with a maximum operating temperature of 1100 °C or 314 grade stainless steel with a maximum operating temperature of 1050 °C.
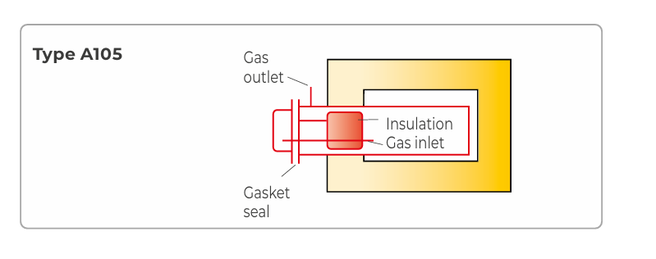
The A105 retort is sealed by a removable front opening insulated door fitted with a silicone rubber seal. Gas inlet and outlet connections are easily accessible at the front. Oxygen levels down to 30 ppm are achievable. A105 retorts for CWF furnaces are fitted with a 3 mm thermocouple gland through the centre of the door. The retort and furnace must be ordered together as the furnace is modified to allow it to be used with, and without, the retort. The A105 retort can be used in combination with the laboratory gas safety system for safe use with hydrogen.
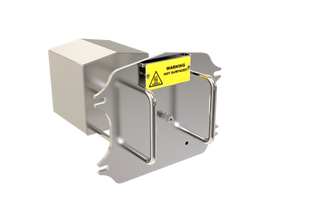
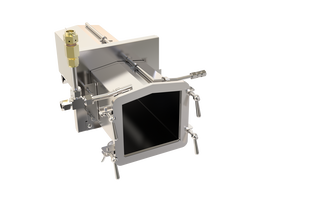
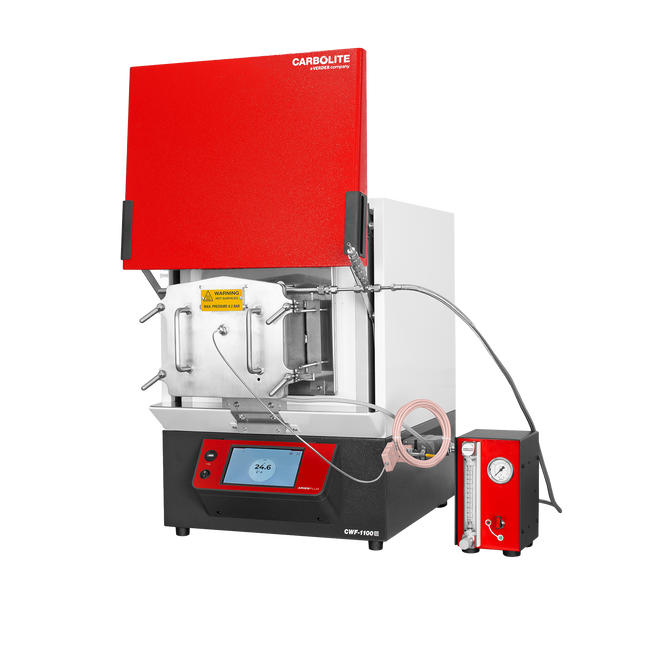
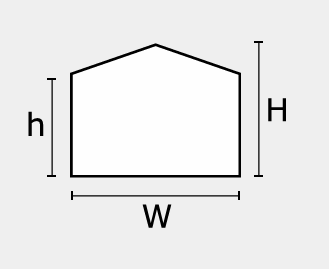
A105 内寸
| CG H Model | Height h/H [mm] |
Width W h/H [mm] |
Depth [mm] |
Door type | ||||
| CWF_/13 | 135/150 | 150 | 275 | pull out | ||||
| CWF_/23 | 170/185 | 195 | 350 | pull out | ||||
| CWF 12/36 | 180/200 | 270 | 400 | pull out | ||||
| CWF 12/65 | 200/225 | 335 | 540 | pull out | ||||
CWF - 汎用卓上型チャンバー炉(電気炉) 1100°C, 1200°C, 1300°C 例
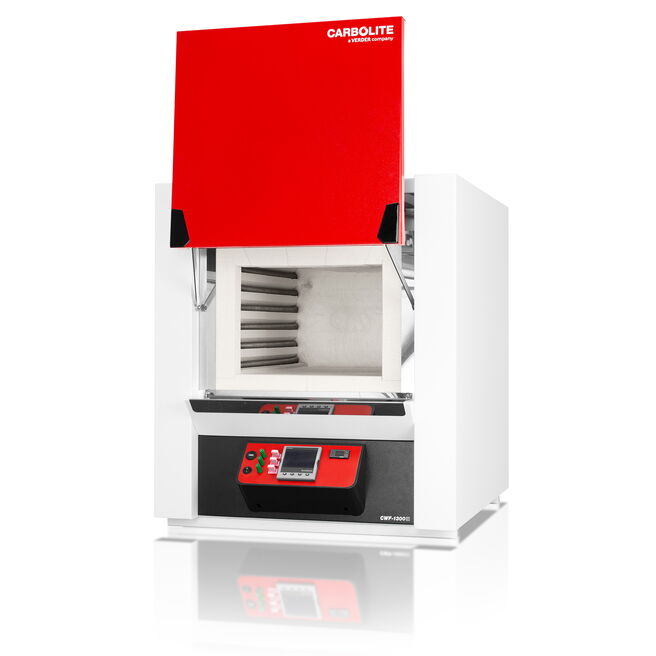
CWF 13/65(ナノダック温度コントローラ付き)
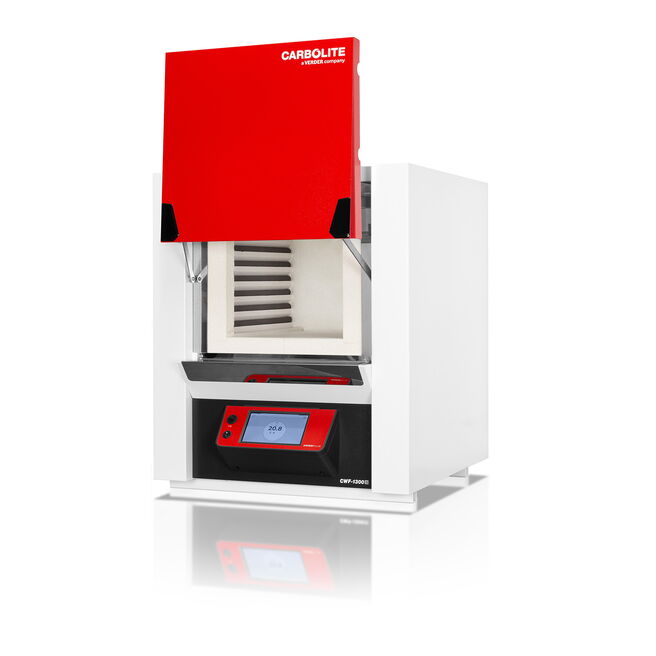
CWF 13/36 牡羊座プラス温度調節器付き
CWF - 汎用卓上型チャンバー炉(電気炉) 1100°C, 1200°C, 1300°C 製品仕様
| 最高温度(℃) | 昇温時間 (分) | 常用使用最高温度 | 寸法: 炉内 H x W x D (mm) | 寸法: 外形 H x W x D (mm) | 寸法: ドア開閉時 H x W x D (mm) | 温度分布(±5℃)均熱部範囲 | 炉内容積 (L) | 最大電力 (W) | 保持電力 (W) | 熱電対タイプ | 重量 (kg) | |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| CWF 11/5 | 1100 | 47 | 1000 | 135 x 140 x 250 | 595 x 375 x 495 | 810 x 375 x 540 | 85 x 90 x 110 | 5 | 2400 | 790 | R | 30 |
| CWF 11/13 | 1100 | 76 | 1000 | 200 x 200 x 325 | 670 x 435 x 608 | 915 x 435 x 675 | 120 x 120 x 185 | 13 | 3100 | 1500 | R | 47 |
| CWF 11/23 | 1100 | 36 | 1000 | 235 x 245 x 400 | 715 x 505 x 680 | 1000 x 505 x 765 | 155 x 165 x 285 | 23 | 7000 | 1900 | R | 68 |
| CWF 12/5 | 1200 | 51 | 1100 | 135 x 140 x 250 | 595 x 375 x 495 | 810 x 375 x 540 | 85 x 90 x 125 | 5 | 2400 | 850 | R | 30 |
| CWF 12/13 | 1200 | 88 | 1100 | 200 x 200 x 325 | 670 x 435 x 608 | 915 x 435 x 675 | 120 x 120 x 200 | 13 | 3100 | 1550 | R | 47 |
| CWF 12/23 | 1200 | 45 | 1100 | 235 x 245 x 400 | 715 x 505 x 680 | 1000 x 505 x 765 | 155 x 165 x 325 | 23 | 7000 | 2250 | R | 68 |
| CWF 12/36 | 1200 | 37 | 1100 | 250 x 320 x 450 | 810 x 690 x 780 | 1105 x 690 x 780 | 170 x 240 x 357 | 36 | 9000 | -- | R | 100 |
| CWF 12/65 | 1200 | 40 | 1100 | 278 x 388 x 595 | 885 x 780 x 945 | 1245 x 780 x 945 | 178 x 288 x 455 | 65 | 14000 | -- | R | 165 |
| CWF 13/5 | 1300 | 75 | 1200 | 135 x 140 x 250 | 595 x 375 x 495 | 810 x 375 x 540 | 85 x 90 x 150 | 5 | 2400 | 1000 | R | 30 |
| CWF 13/13 | 1300 | 121 | 1200 | 200 x 200 x 325 | 670 x 435 x 608 | 915 x 435 x 675 | 120 x 120 x 225 | 13 | 3100 | 1800 | R | 47 |
| CWF 13/23 | 1300 | 55 | 1200 | 235 x 245 x 400 | 715 x 505 x 680 | 1000 x 505 x 765 | 155 x 165 x 340 | 23 | 7000 | 2500 | R | 68 |
| CWF 13/36 | 1300 | 47 | 1200 | 250 x 320 x 450 | 810 x 690 x 780 | 1105 x 690 x 780 | 170 x 240 x 400 | 36 | 9000 | -- | R | 100 |
| CWF 13/65 | 1300 | 55 | 1200 | 278 x 388 x 595 | 885 x 780 x 945 | 1245 x 780 x 945 | 178 x 288 x 255 | 65 | 14000 | -- | R | 165 |
CWF - 汎用卓上型チャンバー炉(電気炉) 1100°C, 1200°C, 1300°C 資料ダウンロード
Cement Testing for Compliance
The compliance of cement with standards such as EN 197 / ASTM C 150 is a quality requirement. Quality assurance of the raw materials used in calcination and also during the clinker production is necessary. Carbolite Gero offers different furnaces that help to guarantee quality requirements are met during the production cycle.
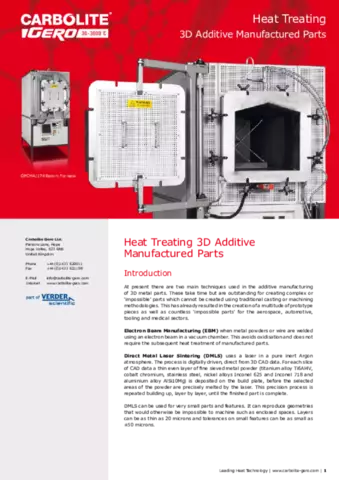
Heat Treating 3D Additive Manufactured Parts
At present, there are two main techniques used in the additive manufacturing of 3D metal parts, Electron Beam Manufacturing (EBM) and Direct Metal Laser Sintering (DMLS). These take time but are outstanding for creating complex or ‘impossible’ parts which cannot be created using traditional casting or machining methodologies. This has already resulted in the creation of a multitude of prototype pieces as well as countless ‘impossible parts’ for the aerospace, automotive, tooling and medical sectors.